 Stage 01
Precision CNC Cutting
Extruded aluminum profiles are cut on automated dual-head CNC saws. Laser measurement tools ensure length and miter angle tolerances within ±0.5mm, creating seamless 45-degree frame corners.
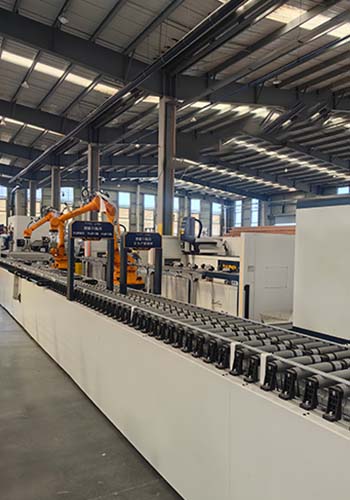
At Foshan Aluvoy Entry Door Systems Co., Ltd., we maintain total control over every step of production in our own facility. By adhering strictly to AS2047, NFRC, and Florida Product Approval manufacturing standards, we deliver structural durability, airtight sealing, and smooth operation on every project.
Stage 01 Extruded aluminum profiles are cut on automated dual-head CNC saws. Laser measurement tools ensure length and miter angle tolerances within ±0.5mm, creating seamless 45-degree frame corners.
 Stage 02
High-speed CNC machining centers mill lock body pockets, hinge slots, hardware mounting points, and weeping channels. Every cut follows detailed CAD/BIM shop drawings for accurate site fitting.
 Stage 03
Dedicated hydraulic punching equipment prepares clean, burr-free drainage ports, corner key locks, and multi-point lock latch cutouts without distorting structural profile walls.
 Stage 04
Corner keys are inserted into the extruded chambers and jointed using German corner crimping technology. Continuous EPDM weather seals and multi-point locking hardware are systematically fitted.
 Stage 05
Dual-component structural sealant is injected into every corner joint. This creates a permanent waterproof barrier and increases frame shear strength under severe wind loads.
 Stage 06
Every frame unit undergoes 5-layer protective wrapping: protective film, foam edge guards, shrink wrap, and solid wooden crates or steel transport racks to ensure safe container transport.
Our quality management system verifies every unit before it leaves the workshop line, reducing field issues and protecting project timelines.
Spectrometer and thickness checks verify aluminum alloy grade (6063-T5/T6) and powder coat layer thickness (≥60 microns) before cutting begins.
Frame and sash dimensions are measured against approved shop drawings. Diagonal tolerance is kept within 1.5mm to prevent operational binding.
Randomly selected production units undergo mock-up testing for water penetration resistance and structural air leakage per AS4420 and ASTM standards.
Operators perform manual cycle tests on friction hinges, multi-point locks, and roller assemblies to confirm whisper-quiet operation and smooth latching.
Real feedback from international buyers who rely on our factory production quality.

"We installed the window and door units on site and were extremely impressed with the corner joint accuracy and finish quality. Thank you for your rigorous work."

"The shipment arrived right on schedule. Unpacking was seamless because the protective crates kept everything pristine. Great job by the production team."

"The engineering precision on these thermally broken sliding doors is top-notch. Our client is extremely pleased with the thermal insulation performance."
Send your elevation plans and window schedules to [email protected] for a fast shop drawing and quote review.